Potato Raw Spirit
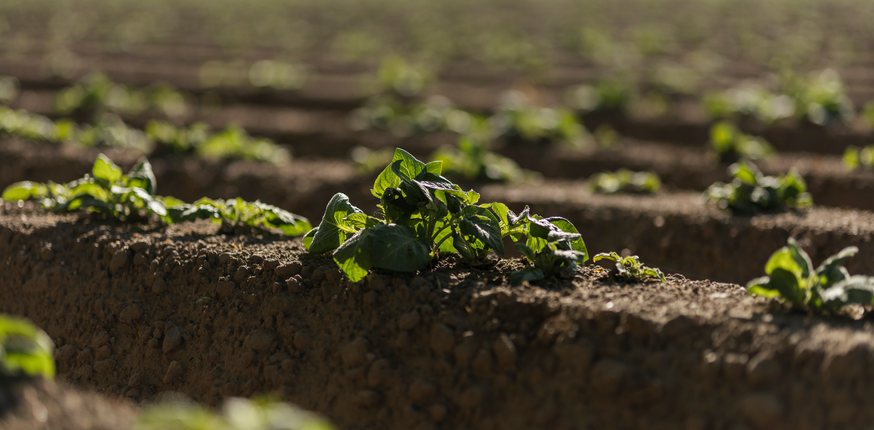
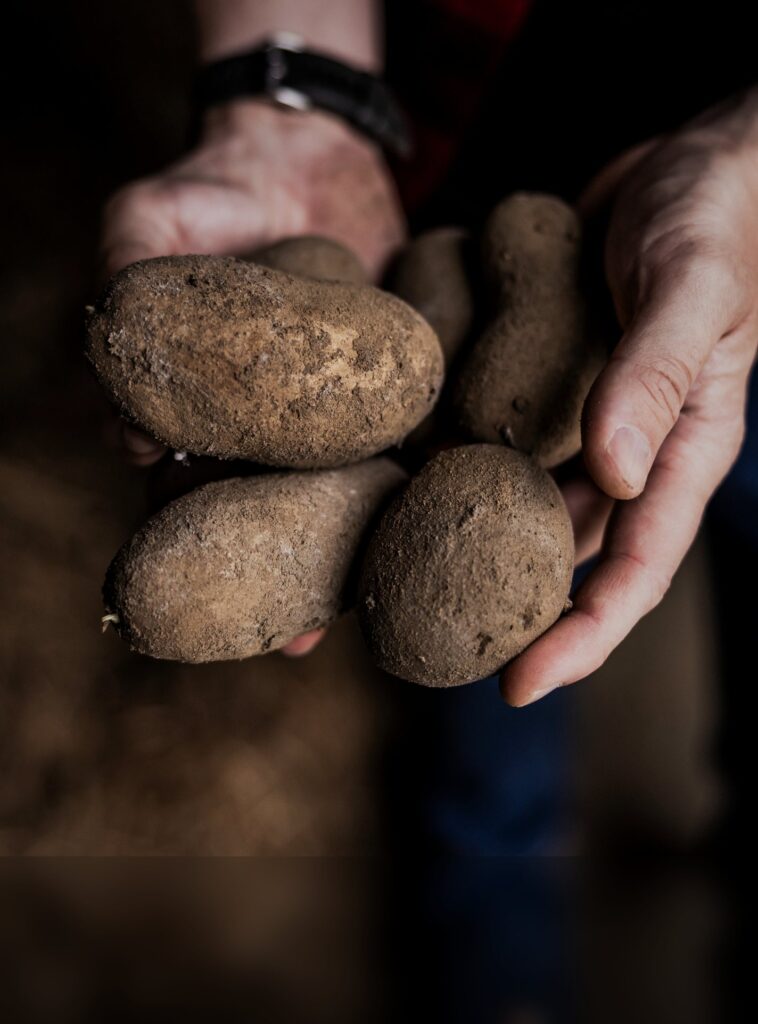
Raw potato spirit for rectification plants and premium alcohol producers. Appreciated by our partners for its consistent availability and reliable quality, thanks to a precisely controlled production process. Every liter comes from one raw material – potatoes grown and processed in Poland.
Learn more
the ideal base for
Product
1/3
Re
Rectifying
01
Product
2/3
Ha
Hard liquor
02
Product
3/3
Fo
For your own distillate
03
We produce 100% potato spirit, without any grain additives. There is no wheat, corn or any other grain in the mash. We are a guarantee of reliability for our customers.
We have proven repeatability of distillate parameters. Each batch is tested chromatographically and sensorily in our own laboratory. The analysis covers methanol, aldehydes, higher alcohols and esters. These are the parameters that matter in further processing.
Alquora spirit contains fermentation by-products, so you can process it as you need – into your own rectified spirit or distillate. For example, it can be the basis of your own neutral alcohol. You can also make a distillate with its own character.
We control the entire process from raw materials, through distillation, to bottling and shipping. You receive full information about the distillate's origin. Should any doubt arise about a batch, we can trace its origin all the way back to the field it came from.
Our standards speak for themselves, but we’re always happy to provide the proof. Order a sample of our distillate. The trial version includes one bottle of raw potato spirit.
ORDER A FREE SAMPLE
Alcoholic beverages made from potato raw spirit account for less than 1% of global production. Our distillate is more than just a technological decision. With this niche product, you can gain a real competitive advantage and attract customers’ attention. Spirit made from potatoes is sometimes called a niche within a niche.
The story of spirit from a traditional Polish distillery is something you can use in your marketing communications to differentiate your product from hundreds of other grain-based alcohols. The raw material is part of the story. We can document its history from the field to the tanker.
01
Our potato spirit is a larger investment, but it will set you apart in the market. With high excise and production costs, the price difference in the final product is marginal.
02
Our distillate meets the regulatory requirements for importing alcohol. We provide complete documentation in accordance with local law so that your product is ready to enter any market. According to US federal rules, ethyl alcohol in bulk has a different customs classification than bottled spirits. We prepare the paperwork for that classification.
03
Alquora Raw™potato agricultural distillate
|
year-round | full certificate of analysis (chromatogram and strength) | potato substrates 90%+ from global G.A.P FSA certified farms | traced to supplier or potato supplier group level | entire process from raw material (mashing, fermentation and distillation) powered by 100% renewable electrical and thermal energy |
Industry standard |
seasonal | strength | potato substrates | unspecified | unspecified |
Contact us, and we will answer all your questions.
Whether you are a global producer, medium-sized bottler, or alcohol distributor, we are a reliable business partner regardless of the scale of your operations. Alcohol is a commodity for most suppliers. For us, each batch is related to one crop from one region.
We operate our production lines around the clock, ensuring constant distillate availability throughout the year, regardless of order size. Production runs through the whole year, so the distillate is also available in months of high demand.
Cooperation can start from as little as 1,000 liters. You can try our distillate in your recipes, perform R&D tests, and decide on a permanent contract without financial risk. That is enough alcohol to make a pilot batch and run a full analysis.
We offer annual contracts, currency hedging support, and 30-day payment terms for regular customers. Longer contracts may be agreed individually.
There are no significant price differences across order volumes. The cost per liter of our distillate in pallet containers is similar to that of a full tanker. Buyers in the United States often convert our quotation to a price per pound. The comparison stays the same.
Experience the intersection of modern precision and three generations of distilling heritage. The mash is heated, fermented and then distilled in a continuous column. We control the temperature at every stage to ensure a repeatable profile.
Once you accept the quality of our distillate, we get down to business. Our cooperation focuses on making the start as easy as possible, followed by the execution of the entire order.
Stage
1/4
Yo
Your needs
We determine whether you need a trial order or a permanent contract. We agree on the volume and requirements for transport, customs clearance, documentation, and insurance.
01
Stage
2/4
De
Delivery date
You indicate when you need the distillate, and we present the available options and a schedule that guarantees efficient order fulfillment.
02
Stage
3/4
Do
Documentation
Once you accept the price and delivery dates, we sign a permanent contract for the supply of potato raw spirit, or you send us a specific order.
03
Stage
4/4
Pr
Production and shipping
After formal confirmation, we start the process. We prepare the selected volume and handle all logistics for the order.
04
Check out the certificates that confirm the safe and ethical origin of our spirit. Health and food safety standards apply to the crop from the field onwards, long before it reaches the distillery.
An international certificate for farms confirming responsible potato cultivation and compliance with food safety standards.
Confirmation that all of our distillate production is completely kosher and complies with specific cultural and dietary rules.
Our agricultural distillery in Pomerania has been operating for over 170 years. We continue to build on the experience and work ethic of our predecessors, improving the production of potato spirit every day. Its history had time to shape the process.
Solutions
1/4
C2
Safety certificates
Solutions
2/4
H5
Historic distillery
Solutions
3/4
O
Expected product quality
Solutions
4/4
H
Holistic approach
Fill out the form below, and we will contact you within one business day. During the conversation, we will discuss:
We have prepared answers to the most frequently asked questions.
Potato raw spirit is an alcoholic beverage produced by the fermentation of potato starch mash. It contains more natural aromatic compounds, has a slightly lower alcohol content (90-93%), and does not undergo rectification. In beverages, ethyl alcohol is the primary type of alcohol, and here the key difference is that raw spirit remains less refined while neutral potato spirit is further purified. Raw spirit is commonly known as an intermediate product rather than a finished alcohol, and it is sometimes called raw distillate. Its chemical profile still carries the compounds that rectification removes. Neutral potato spirit is produced through further distillation and purification, giving it a neutral aroma and exceptional clarity. Neutral spirit is also known as rectified spirit, or simply called ENA. That is a specification, not an absence of character.
Production begins with potatoes, which are crushed and mashed to release simple sugars. The starch is heated with water until it breaks down into sugar. The mash is then transferred to a fermenter, where yeast converts the sugars into alcohol. The liquid at this stage is similar to a strong, unhopped beer, but unlike beer it is never intended for drinking. After fermentation is complete, the mash is distilled to separate the alcohol from water, sediments and natural fractions. This process requires stable temperatures, precise control, and continuous monitoring. Other raw materials such as wheat, corn or rye may be used in the same way, and spirit made from those raw materials is usually called grain neutral spirit. Our production is based on potato and nothing else, and each raw material leaves its own particular mark on the final product.
Typically, the raw potato spirit from the first run of the process reaches an alcohol content of 90-93%. That is the strength of the raw distillate before any further purification. The final parameter depends on the product’s intended use and the customer’s needs.
Yes, in some stages of the process, especially in the final stage of distillation, cold water is used to cool the alcohol vapors and accelerate condensation. This ensures control over temperature, the purity of the fractions, and the stability of the entire system. To use water responsibly, Alquora uses a closed cooling circuit. This reduces groundwater consumption by over 80%. According to our measurements, the same water is heated and cooled many times in the closed circuit.
No. Potato distillate is only a semi-finished product that can be used as a base for further purification. You cannot make vodka from it directly. Alquora neutral spirit is an excellent choice for the production of alcohol, including vodka, liqueurs, and cocktails.
We do not add glucose or simple sugars. Sugars are produced naturally during the breakdown of potato starch during the mash-heating process. As a result, the raw spirit retains its natural profile, contains no masking substances, and guarantees the declared origin. No sugar is added at any stage, and nothing is added later to correct the profile. The sugar in the mash comes only from the starch in the potato. Where a buyer needs proof, analysis by the C13 isotope method can confirm the raw material and rule out cheaper additives.
The difference is due to the price of the raw material, which is the main cost factor in production. A kilogram of starch contained in potatoes is significantly more expensive than in grains. A pound of potato starch costs more than the same weight of corn or wheat starch. The excise, however, is equally high for both. The costs of processing the raw material to prepare it for fermentation are also higher. Nevertheless, the cost of the raw material is usually marginal compared to excise duty or transport costs, so the final price difference for the vodka producer is symbolic. In practice, the raw material is only one part of a much longer cost list for an alcohol importer. The combination of freight and excise makes a bigger difference, even on a full tanker. Pure alcohol for pharmaceutical or industrial applications follows different purity requirements than this production process.